Metal Poured.
Perfectly
Cast.
From liquid metal to precision components — our foundry operations combine decades of casting expertise with modern process control to deliver castings that meet the most demanding industrial specifications.
Where Molten Metal Meets Mastery.
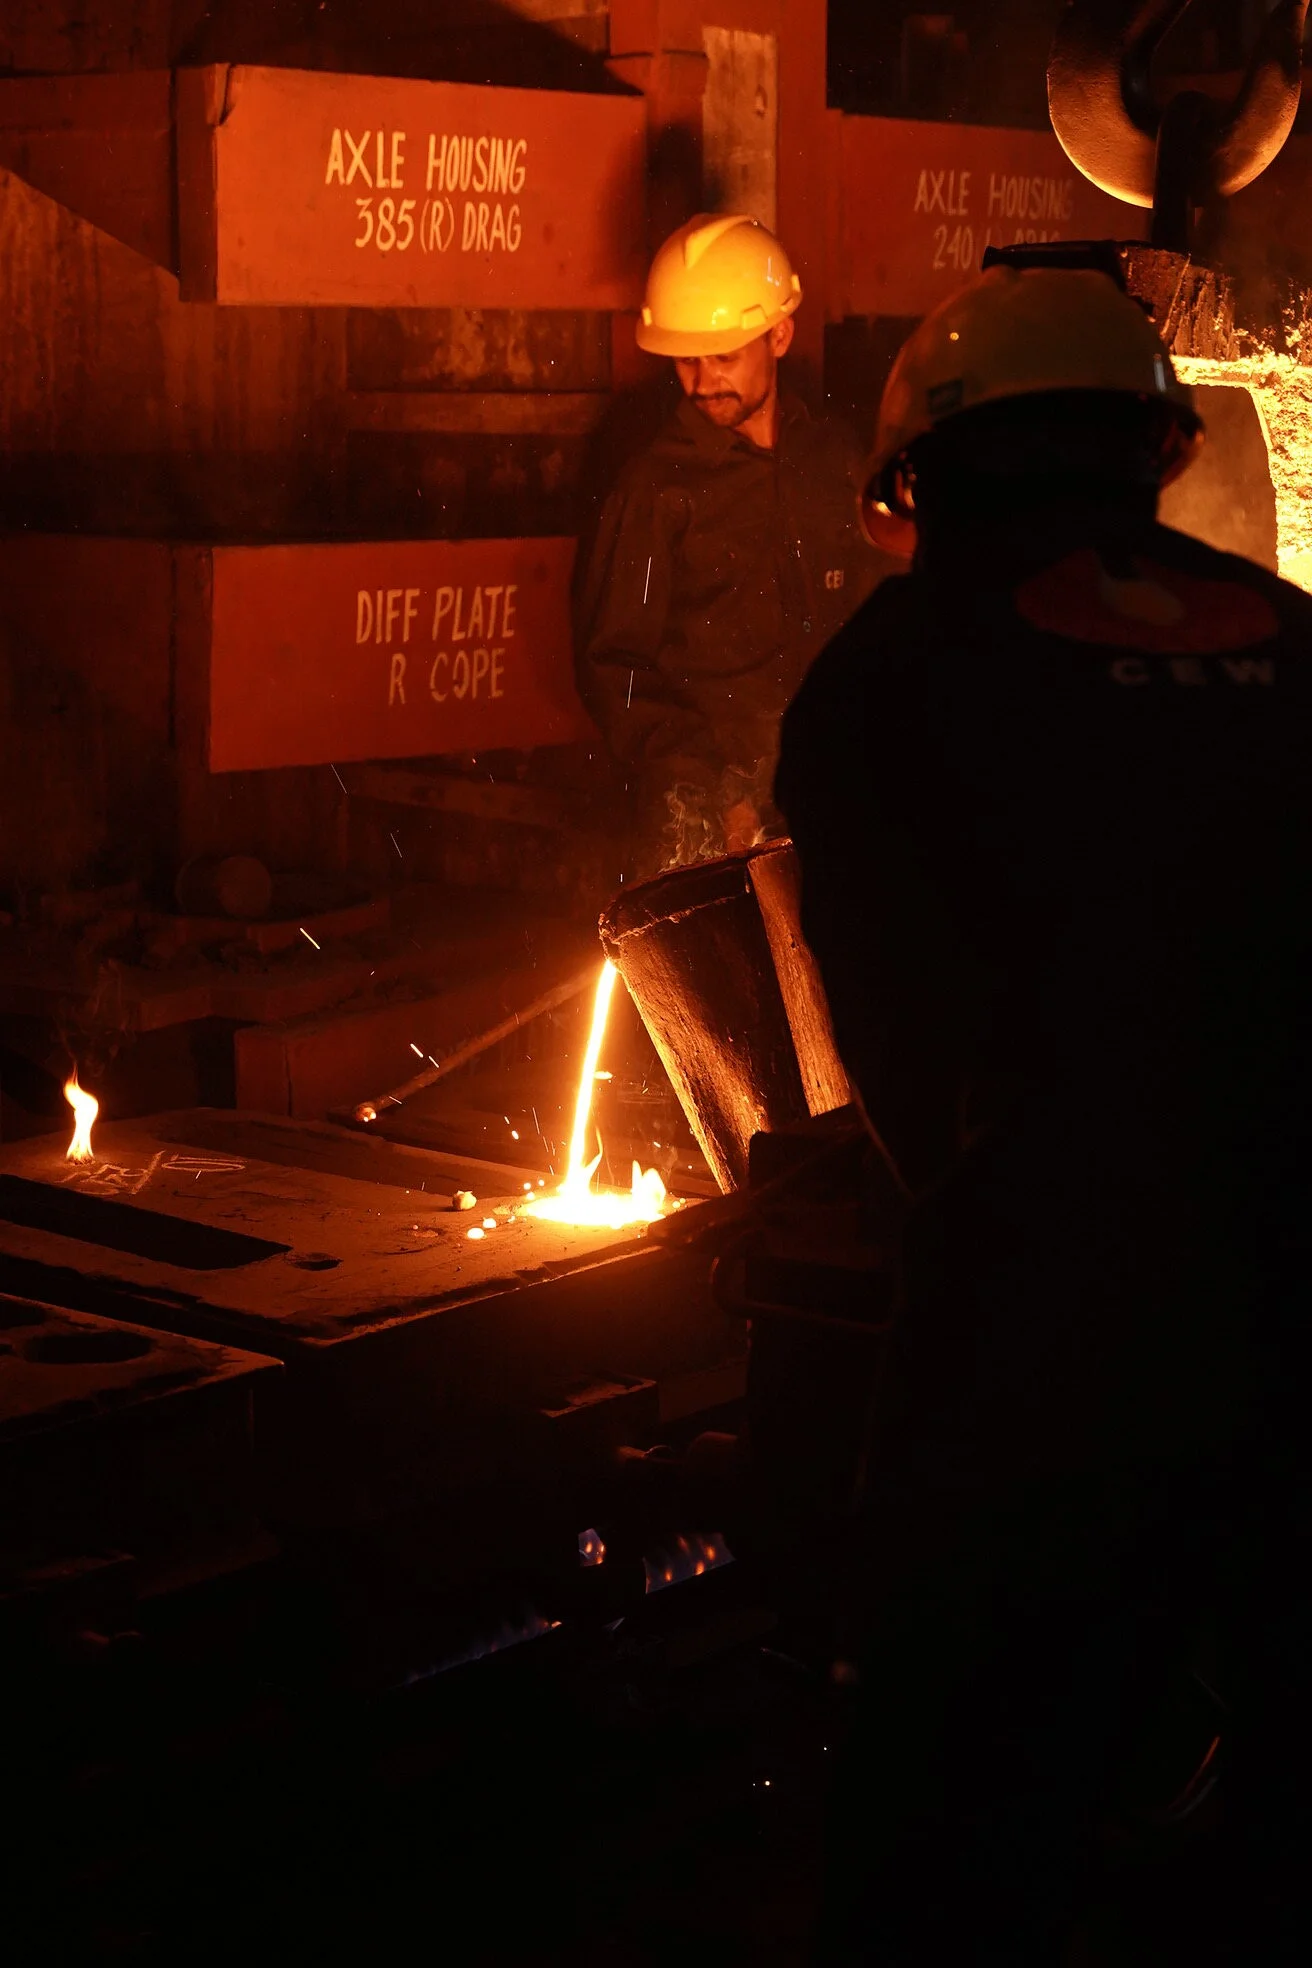
In metalworking, casting is the process in which liquid metal is poured into a mould containing a hollow cavity of the desired shape, then allowed to cool and solidify. The solidified part — known as a casting — is ejected or broken out of the mould to complete the process. Casting is most often used for making complex shapes that would be difficult or uneconomical to produce by any other method. At Chenab Engineering Works, we have refined this ancient process with modern science, delivering castings that perform to the highest engineering standards across a broad range of industrial applications.
Expendable & Non-Expendable Casting Methods
The modern casting process is subdivided into two main categories: expendable and non-expendable casting. These are further broken down by mould material — such as sand or metal — and pouring method, including gravity, vacuum, or low pressure.
Casting processes have supported industrial manufacturing for generations. At Chenab Engineering Works, proven sand-moulding methods are strengthened by modern process control, material verification, and disciplined production standards.
- Green sand and resin sand moulding
- Shell moulding for complex geometries
- CO₂ process for high-strength moulds
Casting Processes & Capabilities
| Process | Available | Suitable Materials | Weight Range | Surface Finish |
|---|---|---|---|---|
| Green Sand CastingExpendable Mould | Grey Iron, Ductile Iron, Steel | 0.5 kg – 2,000 kg | Ra 12.5–25 µm | |
| Resin Sand CastingNo-Bake Process | Alloy Steel, Carbon Steel | 5 kg – 5,000 kg | Ra 6.3–12.5 µm | |
| Shell MouldingSemi-Permanent | Grey Iron, Ductile Iron | 0.1 kg – 100 kg | Ra 3.2–6.3 µm | |
| CO₂ Sand ProcessSodium Silicate | Carbon Steel, Alloy Steel | 10 kg – 3,000 kg | Ra 6.3–12.5 µm |
The Right Alloy for Every Application
Selecting the correct alloy is as critical as the casting process itself. Our metallurgical team works with clients to specify the optimal material grade for each component — balancing mechanical properties, corrosion resistance, machinability, and cost-effectiveness.
From standard grey iron and ductile iron to high-alloy steels, stainless grades, and aluminium alloys, our foundry handles a broad metallurgical range with full composition verification via in-house OES spectrometry.
- Grey iron (GG-20 to GG-35), Ductile iron (GGG-40 to GGG-70)
- Carbon steel and low-alloy steel castings
- Stainless steel (304, 316, 410, 17-4PH)
- Aluminium alloys (A356, A380, LM6)
Our Foundry
Process
A disciplined five-stage casting workflow — from pattern and mould preparation through pouring, cooling, finishing, and final inspection.
Pattern & Mould Prep
Pattern inspection, sand mixing, mould making, and core preparation to exact dimensional specifications.
Melting & Alloying
Precise charge calculation, furnace melting, and alloy adjustment with real-time spectrometric verification.
Pouring & Solidification
Controlled metal pouring at optimised temperature, followed by monitored cooling to minimise defects.
Shakeout & Fettling
Mould breakdown, runner and riser removal, shot blasting, and surface preparation of the raw casting.
Inspection & Dispatch
Dimensional inspection, NDT testing, mechanical testing if required, and final quality release for dispatch.
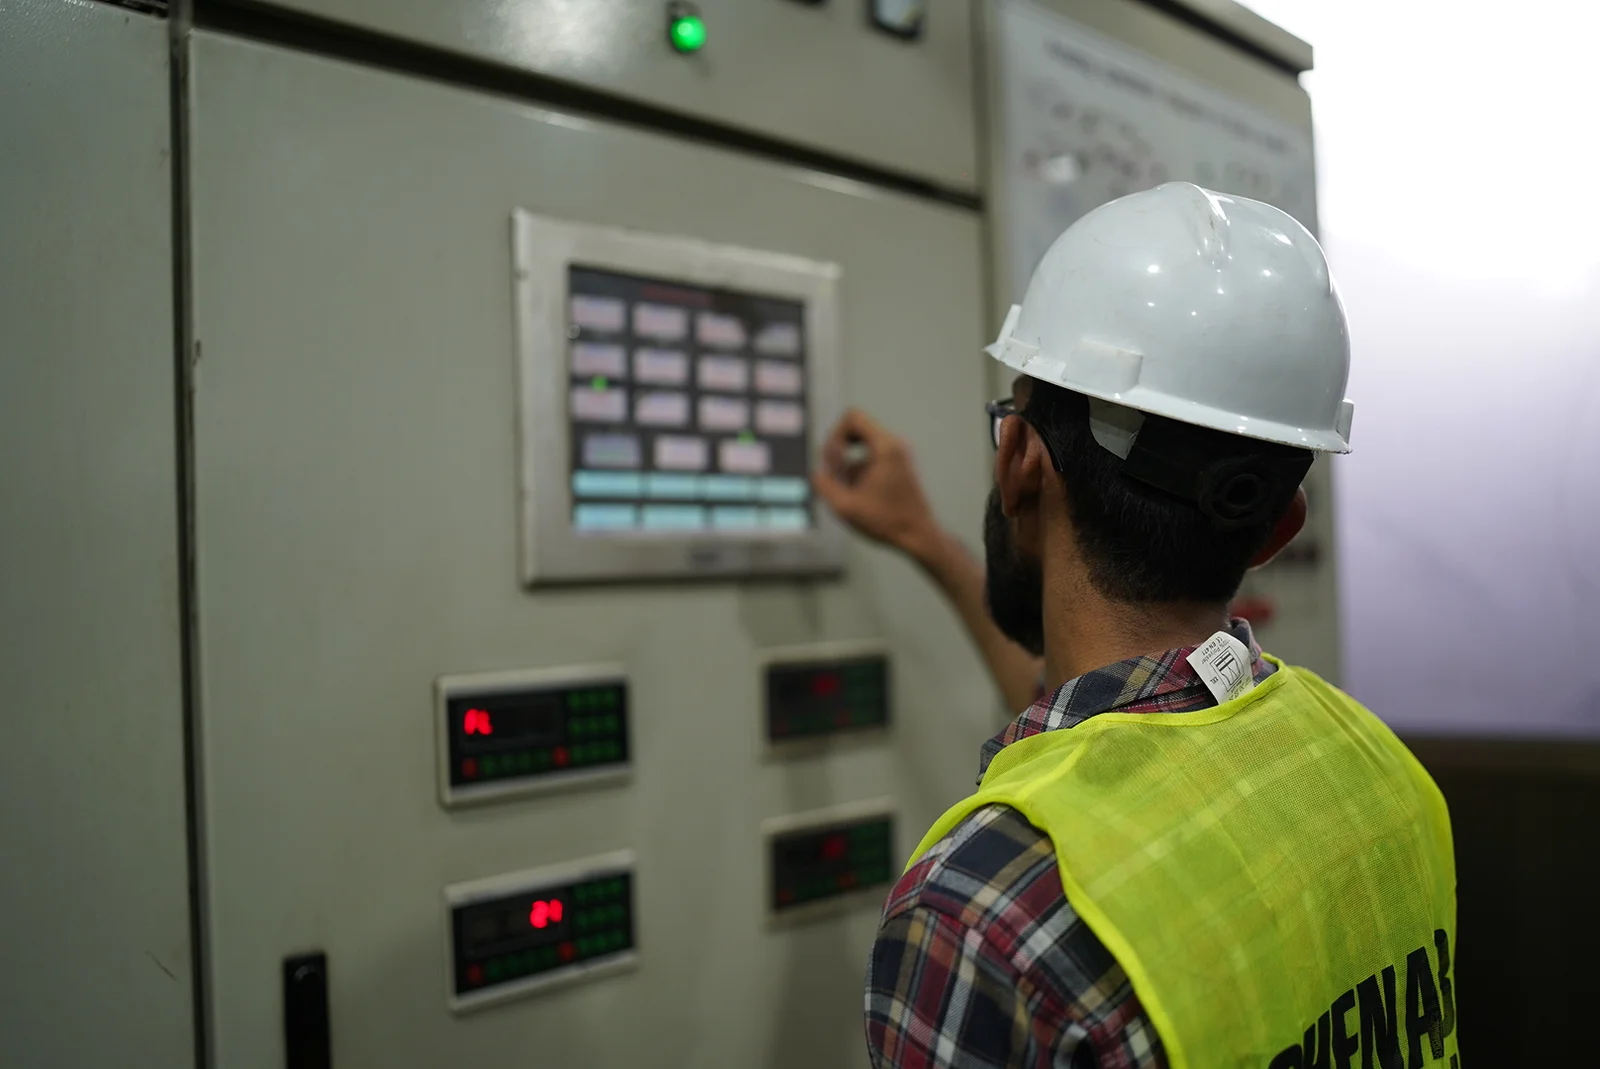
Science Behind Every Pour
Quality at Chenab Engineering Works begins long before metal enters the mould. Our dedicated sand testing, metal analysis, and mechanical test laboratories operate continuously alongside foundry production — ensuring every variable is controlled and every pour is verified.
In-house OES spectrometry provides instant chemical composition data, while our sand lab monitors permeability, compressive strength, and moisture content to maintain consistent mould quality across every shift.
Alloys & Specifications at a Glance
| Material | Category | Applicable Standard | Typical Application | Status |
|---|---|---|---|---|
| Grey Iron | Ferrous | BS EN 1561 | Housings, brackets, machine beds | Active |
| Ductile Iron | Ferrous | BS EN 1563 | Gears, crankshafts, valve bodies | Active |
| Carbon Steel | Ferrous | ASTM A216 | Structural, pressure-containing parts | Active |
| Alloy Steel | Ferrous | ASTM A148 | Heavy machinery and energy components | Active |
| Stainless Steel | Ferrous | Specialist | Marine, chemical, food equipment | Active |
| Aluminium Alloys | Non-Ferrous | BS LM Series | Automotive, aerospace, housings | Active |
Tractor Parts Catalogue
Precision-engineered cast iron and machined tractor components for Massey Ferguson, Fiat, and New Holland models. All parts cast and inspected to exacting quality standards.
Ready to Cast
Something Exceptional?
Partner with Chenab Engineering Works for precise, simulation-validated castings delivered on time — in any alloy, any volume.