Heat Treatment Services in Pakistan
Chenab Engineering Works delivers precision heat treatment services in Pakistan, transforming the hardness, strength, and durability of steel and cast iron through controlled heating and cooling. From hardening and tempering to annealing, normalising, and case hardening, our metallurgists tune every component to its required mechanical properties. Operating computer-controlled atmosphere furnaces at our TÜV Austria certified facility in Faisalabad, we serve agricultural, automotive, defence, and heavy machinery manufacturers nationwide.
Where Heat Becomes Performance.
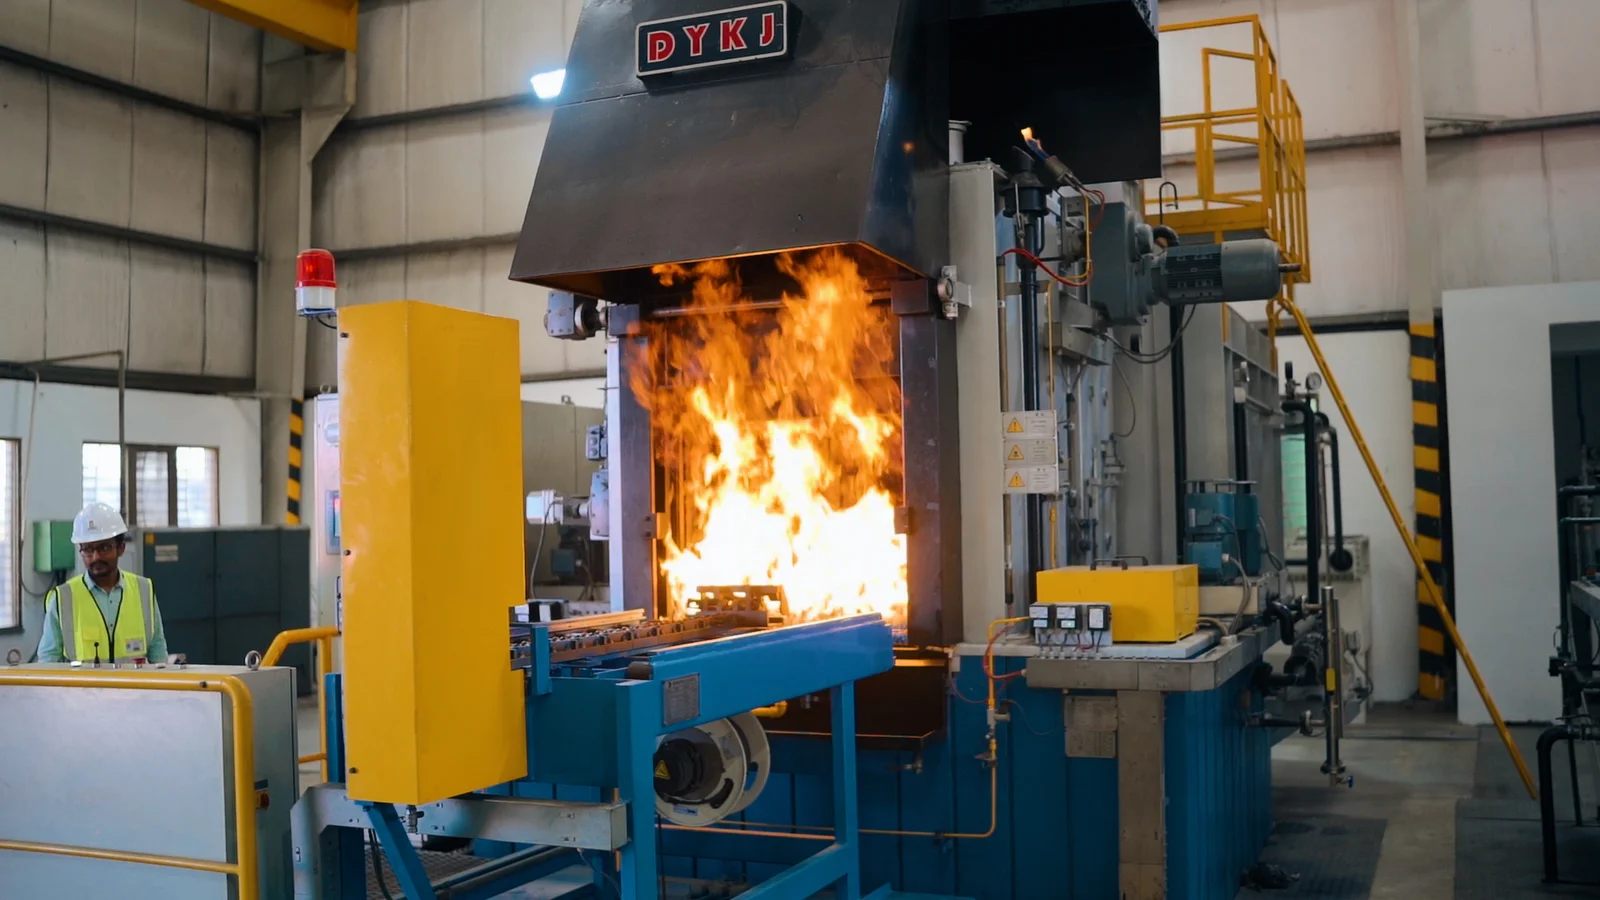
Heat treatment is the controlled process of heating and cooling metals to alter their physical and mechanical properties without changing their shape. By precisely managing temperature, holding time, and cooling rate, the hardness, strength, ductility, toughness, and wear resistance of a component can be engineered to exact specification. The same grade of steel can be left soft enough to machine freely or made hard enough to resist heavy abrasion, depending entirely on how it is treated. At Chenab Engineering Works, we combine decades of foundry metallurgy with modern furnace control to deliver heat treatment that performs reliably under real working loads, from a single prototype to full production batches.
Hardening, Tempering, Annealing & Normalising
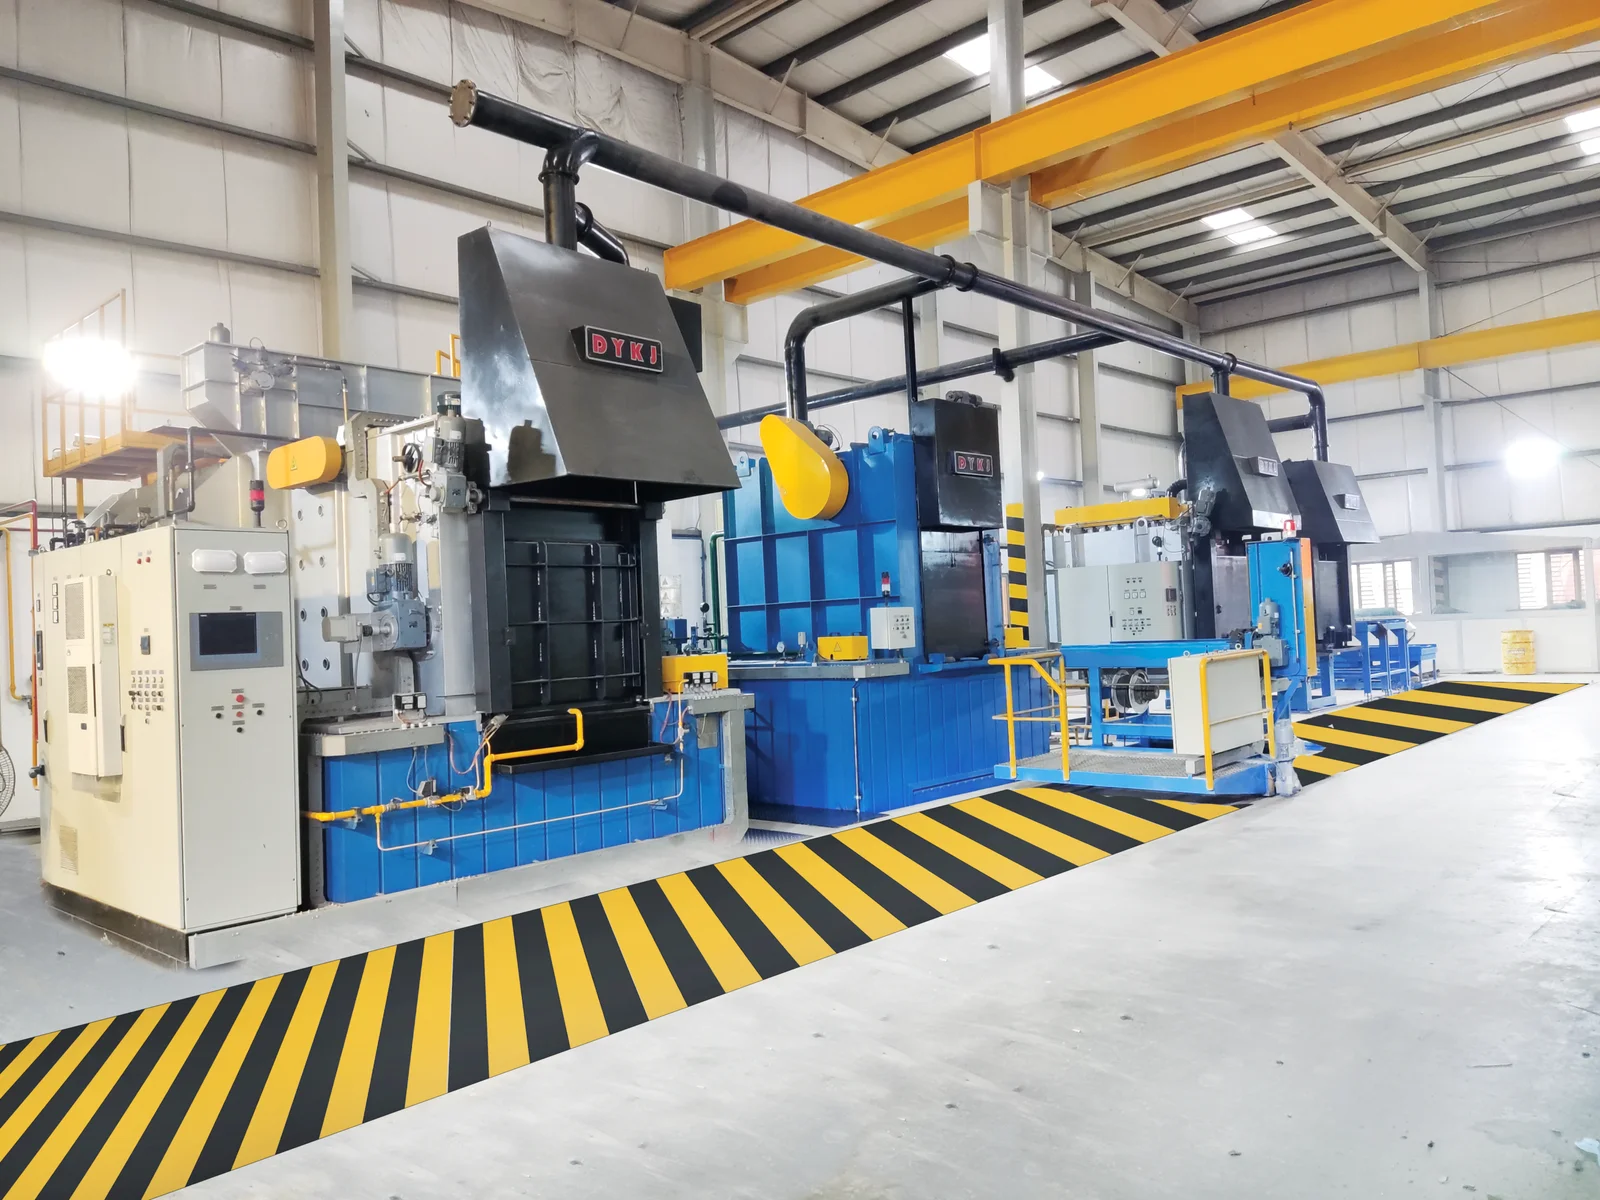
Most heat treatment work is built on a handful of fundamental cycles, each engineered to deliver a specific balance of properties. Hardening raises steel above its critical temperature and quenches it rapidly to lock in a hard martensitic structure, while tempering follows to restore toughness and remove the brittleness that hardening leaves behind.
Annealing softens metal and relieves internal stress for easier machining and forming, and normalising refines the grain structure to give uniform, repeatable mechanical properties across a full batch. Choosing the correct cycle for each component is where metallurgical judgement makes the difference between a part that lasts and one that fails early.
- Through hardening and quenching in oil, water, or polymer
- Tempering for a balanced blend of hardness and toughness
- Full and process annealing for machinability and ductility
- Normalising for uniform, fine-grain structure
- Stress relieving for welded, machined, and cast parts
Heat Treatment Processes & Capabilities
| Process | Available | Suitable Materials | Typical Temperature | Outcome |
|---|---|---|---|---|
| Hardening & QuenchingThrough Hardening | Carbon & Alloy Steel | 820 to 900 °C | Up to 60 HRC | |
| TemperingToughening Cycle | Hardened Steel | 150 to 650 °C | Toughness restored | |
| Full AnnealingSoftening | Steel & Cast Iron | 700 to 900 °C | Soft and machinable | |
| NormalisingGrain Refinement | Carbon & Alloy Steel | 850 to 950 °C | Uniform grain | |
| CarburisingCase Hardening | Low-Carbon Steel | 880 to 950 °C | Hard case, tough core | |
| Induction HardeningSurface Hardening | Medium-Carbon Steel | Surface localised | 50 to 62 HRC | |
| Stress RelievingDistortion Control | Welded & Cast Parts | 550 to 680 °C | Residual stress reduced |
A Hard Surface Over a Tough Core
Many components must resist surface wear while staying tough enough to absorb shock and fatigue. Case hardening achieves exactly this, diffusing carbon or nitrogen into the outer layer to create a hard, wear-resistant skin over a ductile core. Gears, shafts, cams, sprockets, and tractor linkage pins are typical candidates.
We offer carburising, carbonitriding, and induction hardening, each suited to different geometries, material grades, and performance requirements. Induction hardening delivers targeted surface hardness while case depth is controlled to the drawing specification.
- Carburising and carbonitriding for low-carbon steels
- Induction hardening for shafts, gear teeth, and pins
- Flame hardening for large or localised surfaces
- Controlled case depth to exact drawing specification
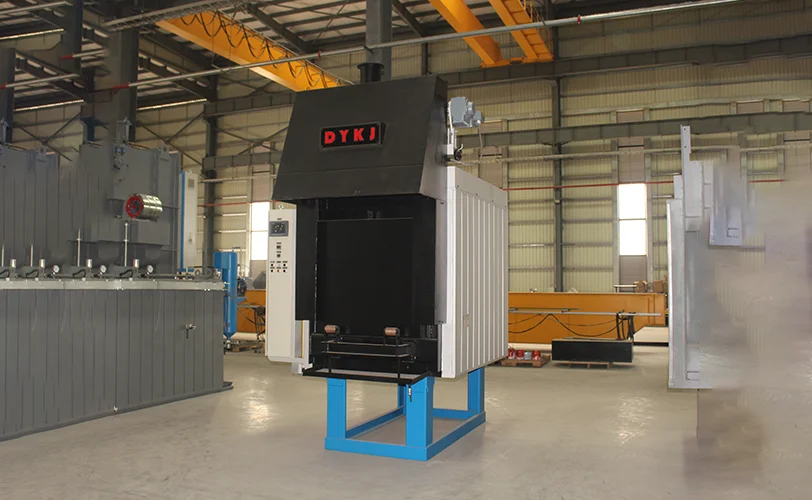
Our Heat
Treatment Process
A disciplined cycle from incoming inspection and material verification through controlled heating, quenching, tempering, and final hardness validation, fully documented at every stage.
Material Verification
Incoming inspection, grade confirmation, and review of the required specification, target hardness, and case depth.
Controlled Heating
Loading into atmosphere-controlled furnaces and heating to the precise austenitising or process temperature.
Quenching
Rapid, uniform cooling in the correct medium, oil, water, polymer, or air, to develop the target microstructure.
Tempering & Relieving
Reheating to relieve stress, restore toughness, and dial in the final balance of hardness and ductility.
Hardness & Inspection
Rockwell, Brinell, or Vickers testing, case depth checks, and full certification before dispatch.
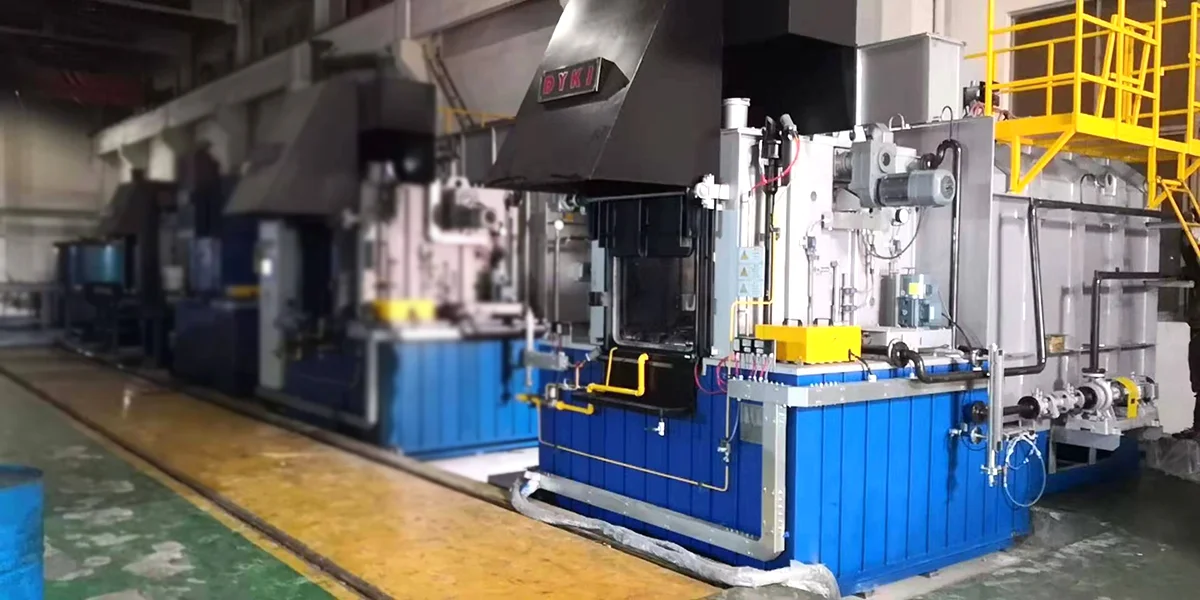
The Science Behind Every Cycle
Repeatable heat treatment depends on data, not guesswork. Our metallurgical laboratory monitors furnace temperature uniformity, quench performance, and atmosphere composition on every batch, so the results stay consistent from the first part to the last.
Hardness testing across the Rockwell, Brinell, and Vickers scales, combined with microstructure examination and case depth measurement, confirms that each component meets its specification before it leaves our facility, backed by a full test certificate.
Treatments, Benefits & Applications
| Treatment | Process Type | Typical Hardness | Typical Application | Status |
|---|---|---|---|---|
| Hardening & Tempering | Through Treatment | Up to 60 HRC | Gears, shafts, axles | Active |
| Full Annealing | Softening | 120 to 180 HB | Castings, forgings, billets | Active |
| Normalising | Grain Refinement | 150 to 200 HB | Structural steel parts | Active |
| Carburising | Case Hardening | 58 to 62 HRC case | Pins, bushes, sprockets | Active |
| Induction Hardening | Surface Hardening | 50 to 62 HRC | Shafts, gear teeth, rollers | Active |
| Stress Relieving | Stabilising | Hardness unchanged | Welded & cast assemblies | Active |
Heat Treatment Services FAQs
What heat treatment services do you offer in Pakistan?
How much does heat treatment cost?
Which materials can you heat treat?
What is the difference between hardening and tempering?
Can you achieve a specific hardness or case depth?
Do you provide hardness testing and certification?
Where is your heat treatment facility located?
Tractor Parts Catalogue
Precision-engineered cast iron and machined tractor components for Massey Ferguson, Fiat, and New Holland models. All parts heat treated and inspected to exacting quality standards.
Ready to Harden
Your Components?
Partner with Chenab Engineering Works for precise, certified heat treatment services in Pakistan. From our facility in Faisalabad we serve manufacturers across Lahore, Karachi, and beyond, delivering hardening, tempering, annealing, normalising, and case hardening to exact specification, on time and in any volume.